Inside Cleveland-Cliffs' Middletown Innovation Engine: A Steel Buyer's Field Guide
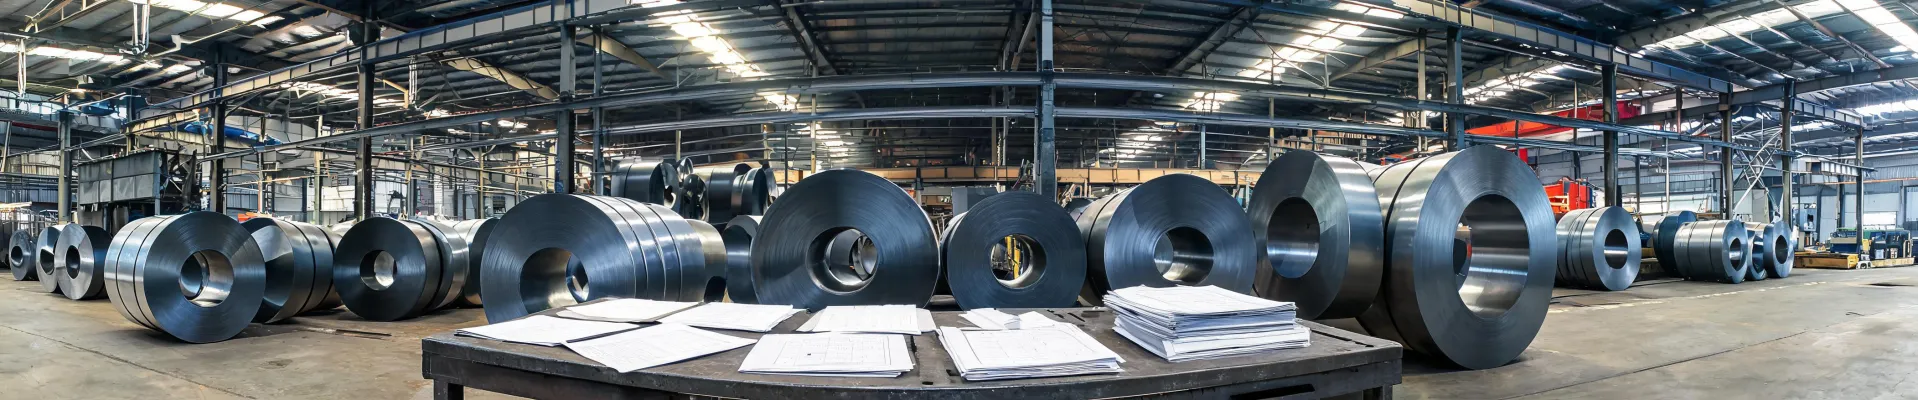
Inside the 135,000-square-foot Research and Innovation Center in Middletown, Ohio, engineers from Cleveland-Cliffs and customer plants share one table. A sheared sample moves hand to hand while someone sketches a forming die on a whiteboard; the argument is about edge quality, coating behavior, and where a part might thin before it splits. This is not a museum of steel grades. It is the centerpiece of a research program, a customer-friendly facility built for joint development projects, and the question underneath every conversation is simple: what does this place mean for the steel you buy?
Inside the 135,000-Square-Foot Test Bed
You have every reason to be skeptical. If your job is buying commodity galvanized coil, a steel supplier that also runs a research center sounds like an extra cost they will pass on to you. But the moment a metallurgist asks about your actual die and coating cycle, the dynamic changes. The conversation turns from price per ton to whether the material will survive your stamping process, your corrosion test, your weld line. A research center only earns its keep when it changes how a supplier responds after a trial part fails. The real question is not whether a mill can roll to a thickness. It is whether the people selling steel treat your production line as the final test of their product. That is the standard a steelmaker should be held to before it earns a place on your approved supplier list.
That building—the 135,000-square-foot Research and Innovation Center in Middletown, Ohio—does not exist in isolation. Cleveland-Cliffs calls it the centerpiece of its research program, and the strategic direction is explicit: shifting away from commodity steel toward higher-margin specialty products. Rather than a guarded corporate lab, the RIC was designed to be customer friendly, with space that facilitates joint development projects between customers, research groups, and operations. A customer can bring a forming issue or corrosion requirement and work directly with metallurgists who also deal with production lines. The result is faster development and faster launch, because mill operations join the conversation before a grade is finalized. The facility also hosts technical symposia and workshops on formability, corrosion, and welding—topics customers actually wrestle with. That working space is the point: trials need room, not just phone calls.
Contrast that with the old commodity formula: buy coil on price, hope the gauge and coating stay inside tolerance, and accept that problem-solving happens after the fact in your own plant. The RIC model turns that sequence around. Because the same company controls the research center and the production lines, development questions do not have to pass through a sales desk; die wear or coating adhesion can go straight to the people who specify the steel. That distinction is not academic. For a part with tight yield and elongation targets, the gap between a commodity batch and a purpose-built specialty grade shows up as scrap, rust, or a failed weld. The shift toward specialty steel aligns incentives: the supplier wants the higher-margin grade to work in your plant. When you see the Middletown address on a quote, ask not 'do they have capacity?' but 'will they let me into the innovation loop early enough?'
From Mine to Finished Coil
Vertical integration at Cleveland-Cliffs starts before the steel is molten. The company is vertically integrated from the mining of iron ore, pellet and direct reduced iron production, and scrap processing, through primary steelmaking and downstream finishing, stamping, tooling, and tubing. One organization owns the loop from raw material to the part that bolts into a vehicle. Self-sufficiency in raw materials is the unusual advantage: a mill that buys ore or scrap on the open market is exposed to price and quality swings. The loop does not stop at the coil: when the same group handles stamping and tooling, feedback from finished parts reaches the steelmaking floor quickly. A forming crack in a trial part becomes a signal about chemistry or cast structure, not a distant complaint. That control is why integration shows up in delivery stability and quality.
What does that vertical reach mean for a buyer planning a 2027 launch? Steel supply surprises reach the factory floor in predictable ways: a scrap price spike closes a competitor's order book, a railroad delay strands a coil, a quality deviation forces a line to re-qualify. An integrated supplier cannot eliminate those events, but it removes uncertainty from depending on someone else's mines and melt shops. More important, the early and late steps are in one organization, so a specification change does not travel through three companies. The sourcing question is not 'can they hit the gauge range?' It is 'if results tell us the steel needs a tweak, who is in the room to make it fast?'
The integration story also carries a carbon accounting advantage. Cleveland-Cliffs says it has reduced carbon emissions by 25%, tracked in a sustainability report aligned with GRI and SASB standards for the iron and steel sector. The company also obtained external limited assurance on its consolidated Scope 1 and Scope 2 greenhouse gas emissions data. For a Tier One supplier with customers who ask for environmental data, that is not decorative: a producer that controls ore, energy, and finishing lines can influence each coil's footprint. A trader of imported steel can only pass along someone else's numbers. The 25% reduction gives your disclosure a verifiable upstream claim, not a promise. It does not make steel green in absolute terms, but it is a place to start. That matters when OEM procurement starts weighting carbon.
The Grade List Gets Specific
Walk through the product lineup and you can see why the company is described as the largest flat-rolled steel producer in North America and the largest supplier of automotive-grade steel in the U.S. The portfolio covers flat-rolled carbon steel, stainless, electrical, plate, long products, carbon and stainless steel tubing, plus hot and cold stamping and tooling. That breadth is deliberate: each family serves a different part of a vehicle or building, and a Tier One buyer can often find the product architecture within one supplier. The list is not an accident; it is the material form of the specialty-steel strategy. It also shortens qualification, because a single technical interface spans families when part requirements change from a galvannealed substrate to an AHSS.
Drill into the catalogs and the structure becomes visible. Cleveland-Cliffs manufactures over 50 stainless steel alloys, and stainless steel contains at least 10.5% chromium, with elements like carbon, manganese, molybdenum, silicon, nickel, titanium, and niobium added to create a range of grades. On the automotive side, the advanced lineup includes third-generation advanced high-strength steels (AHSS), dual-phase hot-dipped galvanized and galvannealed products, multi-phase and complex-phase grades, and press-hardenable or press-quenched steel for structural parts. There are also aluminized and specialty-coated products for corrosion resistance. The 10.5% chromium line is a useful field marker for when a material moves into stainless behavior. Above all, this is not a mill selling one good grade; it spans from a simple carbon coil to an ultra-formable steel for high-speed stamping.
That breadth is not window dressing. A wide portfolio means a demanding customer can often find a solution without changing suppliers, and the supplier can reach new markets without building a new chain. Cleveland-Cliffs points to this as a reason for increased share in automotive and expanded reach into infrastructure, manufacturing, distributors, converters, and steel producers. The causal chain is direct: wide catalog lets you match a forming process or corrosion requirement to a proven grade; the proven grade shortens development risk; shorter risk makes a future launch viable. When issues appear, adjacent grades serve as insurance—something a narrow mill cannot offer. That is a practical advantage, not a marketing phrase.
The Award That Signals Trust
Why trust those capability claims? Capability on paper is cheap; any mill can print a catalog. What separates a marketing page from a real relationship is reliability under purchasing pressure. When a coil misses a coating target and your line stops, you do not want a supplier still figuring out the grade. Structural size can be part of the answer, but size can mask a commodity mindset. The better signal is an external judgment from an automaker that audits suppliers the way engineers audit material certificates. That kind of judgment is hard to fake, because it comes from a customer with its own shutdown risk and quality recall exposure. So a third-party award can be the tie-breaker when two mills offer similar numbers.
Start with market position and treat it as a load-bearing fact. Cleveland-Cliffs says it is the largest flat-rolled steel producer in North America and the largest supplier of automotive-grade steel in the U.S. That scale means satisfying demanding automaker standards across millions of tons, which is not compatible with erratic quality. The description comes with a product scope that includes advanced, high-quality, technologically advanced steel for exacting performance standards. For a practitioner, the translation is simple: the position is a consequence of being chosen again and again, not a prize for being biggest. Size can bring bureaucracy, but in flat-rolled automotive supply, size enables investment in infrastructure like the RIC. So read the market position as a foundation for the specialty story.
Then comes an external check that cuts through marketing. General Motors named Cleveland-Cliffs a 2025 GM Supplier of the Year at its 34th annual event, and the company was the only North American steel producer recognized that year. It was also the ninth time Cleveland-Cliffs had earned the award. GM's supplier awards are not sentimental; they measure quality, delivery, and responsiveness. Nine wins across changing product cycles signal consistency. For a Tier One parts buyer, that external judgment says the integrated model—mines to finished coil plus the RIC—produces outcomes an automaker can measure. That is trust a brochure cannot provide.
Your Field Check Before You Spec
How do you actually test whether a Cleveland-Cliffs solution fits your part? The field check begins before the PO. Name the three risks that keep you awake during a launch: forming splits or thinning, corrosion in a coating system, and weldability across mixed-material joints. Then ask whether the supplier can discuss those failure modes in process language, not just data-sheet language. If the answer to 'what happens when blanking temperature goes up?' is a shrug, you are buying commodity. If the answer includes a trial plan and a referral to the innovation center, you've found a development partner. And test physically: request a sample, run it on your own line, and see whether the supplier treats the result as a shared problem.
The RIC is the physical tool for that check. Its workshop themes—formability, corrosion, welding—line up exactly with those field risks. Cleveland-Cliffs built the facility specifically as customer-friendly space for joint development, which is a different starting point than a typical corporate lab. If you are a process engineer trying to understand how a new AHSS behaves in your die, a workshop beats a stack of data sheets because you are in a room with metallurgists and production engineers. Bring your part geometry, coating questions, or weld schedule; get answers grounded in mill trials. The stated culture is one of innovation and collaboration, where products and processes are developed more efficiently and launched faster. For a 2027 deadline, that speed matters. The real value is not the square footage; it is the habit of treating your forming problem as a development problem.
Step back into the opening image: the 135,000-square-foot room in Middletown where engineers and customers share data around a sample. That image is the field check in capsule form. The steel you buy today comes out of that development loop, and the question that should decide your next spec is not 'how many grades can you list?' It is 'will the supplier invite me into that room while the part can still change?' A supplier who opens the lab door early is treating your launch as its own. The difference shows up in parts that form, weld, and survive—not in brochures. That is what the Middletown name has come to mean.
Keep that door in mind when a certification sheet crosses your desk. The Middletown address on the coil is not a plant locator; it is an invitation to test whether your hardest forming and welding questions get answered in a 135,000-square-foot room built for exactly that purpose.
Ingrid Solberg
Ingrid Solberg is an independent carbon and structural steel analyst covering steel plate, sheet, coil, pipe, beams, rebar, and galvanized products. She applies ASTM A36/A36M and A6/A6M requirements while comparing grade chemistry, yield strength, tensile strength, elongation, dimensional tolerance, weldability, and surface condition. Her evidence-led guides help engineers, fabricators, and procurement teams select suitable steel forms, define purchase specifications, and evaluate mill or service-center offers.