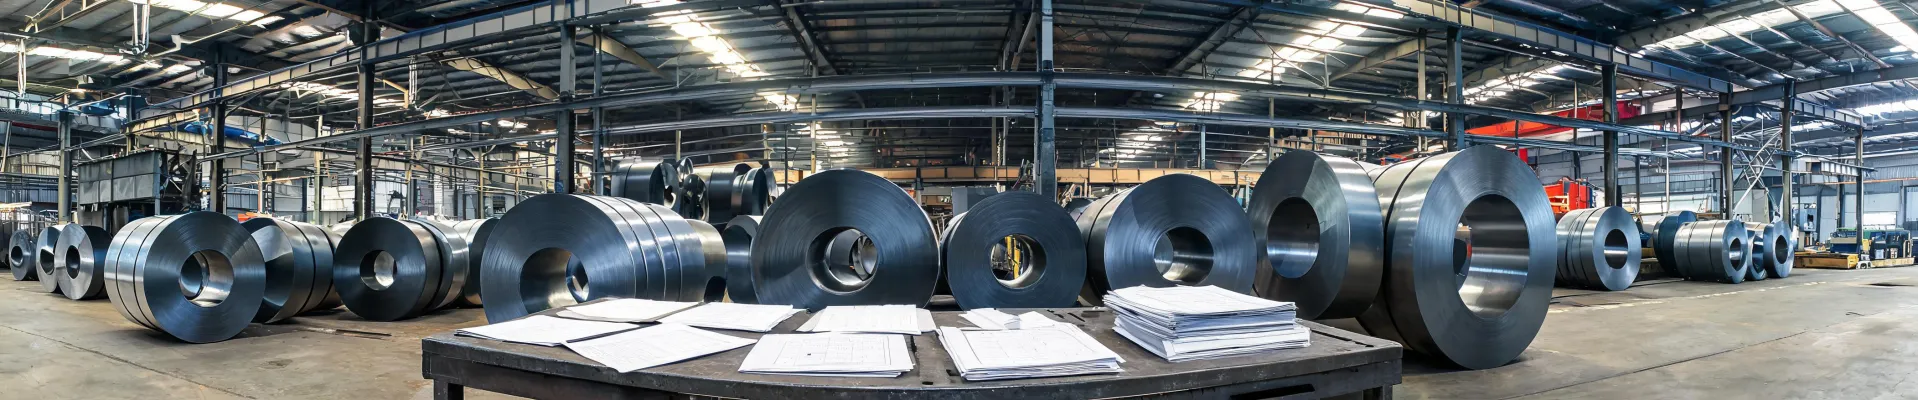
Choosing Grain-Oriented or Non-Oriented Electrical Steel at Zanesville
A wrong electrical steel grade stays invisible at the receiving dock and turns expensive at the test bench. The coil arrives the same size, the same thickness, the same dull gray as the correct one. It shears, stacks, and winds the same way. Then the finished transformer or motor reaches a customer's bench, the core loss reads high, the core runs hot, and the efficiency figure the machine was bought against does not pass. The recovery is measured in weeks of rework and a schedule you already promised to someone else.
One judgment prevents most of that: grain-oriented and non-oriented electrical steel are not two quality levels of the same product. They are two materials matched to the shape of the magnetic field around them. Cleveland-Cliffs finishes both at its Zanesville Works, and the deciding factor is field geometry — a flux path that holds one fixed axis, or one that rotates. The grade name tells you nothing about which you need.
What One Wrong Electrical Steel Grade Costs
What does a wrong grade cost before the first coil is even cut? Nothing yet — and everything, because the mistake is already made in the material specification. Every step after that, from blanking to annealing to stacking to varnish cure, spends real money on the wrong metal. The finishing lines at Zanesville are built to hand customers specialty flat-rolled product that meets their exact specifications and delivery requirements; a mis-specified grade breaks that promise downstream, at your plant rather than at the mill.
A motor shop I worked with tried to buy margin by running a grain-oriented grade into a stator. On the datasheet the loss looked better than the non-oriented sheet it replaced. On the dynamometer the gain evaporated, because a stator's field rotates and keeps swinging away from the one direction that grade is good at. They shipped the first build anyway. Then they paid to strip stators, rewind, re-test, and expedite replacements. The loss figure is the small bill; requalification, scrap, and a late-delivery penalty are the real one.
Electrical Steel Is Not Ordinary Flat-Rolled Steel
What makes electrical steel a different class of material from ordinary flat-rolled steel? Its job is to carry magnetic flux, not load. Silicon sets the chemistry — roughly 3 percent in grain-oriented grades, similar in many non-oriented ones — and that alloying raises electrical resistivity, which starves the eddy currents that would otherwise heat a core at line frequency. Rolling and annealing set the grain structure, because core loss depends on how freely magnetic domains can move.
Plain low-carbon sheet cannot substitute for it. It is stronger, cheaper per tonne, and wrong in a core: too conductive, so eddy currents circulate, and with no controlled texture, so magnetising current climbs and the core cooks. Zanesville brings specialty flat-rolled process and product technology together, which is the part buyers usually miss — the rolling practice and the published grade data are developed as one system, so the magnetic properties hold from coil to coil.
Grain-Oriented vs Non-Oriented Electrical Steels
If both grades are finished on the same site, what actually separates grain-oriented from non-oriented? Texture. Regular Grain-Oriented (RGO) electrical steel, the grade family for power and distribution transformers, offers an outstanding degree of grain orientation: the easy magnetisation axis of nearly every grain is lined up with the rolling direction. Cold-rolled non-oriented (CRNO) electrical steel takes the opposite route — its magnetic properties are practically the same in any direction of magnetism, by design.
Strip away the catalogue language and the split is directional versus isotropic, not premium versus ordinary. RGO is tailored so one axis carries flux with unusually low loss; CRNO is tailored so no axis is left behind. Neither is a higher grade of the other — they are two different contracts with two different flux paths. Same finishing lines, two different jobs.
Why Flux Direction Decides the Grade
So why does the direction of magnetisation decide the grade, and not the loss number on the front of the datasheet? Because flux geometry belongs to the machine, and the machine does not negotiate. In a transformer, flux is essentially one-dimensional and fixed: it enters the core, turns, follows the laminations, and reverses fifty or sixty times a second without ever changing axis. Aligned grains sit right on that path, domain walls move easily, and loss stays low.
A rotating machine is a different geometry. Stator teeth and yoke see flux sweep through a full revolution, so there is no single direction worth optimising — and a grade tuned for one direction is worse in the others than the isotropic sheet it replaced. This is also where datasheets mislead. RGO grades are commonly quoted at 1.7 T while CRNO is often quoted at 1.5 T, so two figures in watts per kilogram are not comparable until you know the induction and frequency behind them.
How to Verify a Coil Meets Its Grade
How do you confirm a delivered coil truly matches the grade you ordered? Start with the mill test certificate, then read what it certifies: specific loss in watts per kilogram at a stated induction and frequency, thickness, coating type, and stacking factor. A grade name on a tag proves nothing. The magnetic test behind those numbers follows a standard — an Epstein frame or a single-sheet tester under IEC 60404-3 or ASTM A804 — and the certificate has to name the induction, or you cannot compare it against your own acceptance limit.
Then watch the batch, not the family average. Two coils can share a grade name and still differ in loss across a heat, and that scatter is what turns a comfortable design margin into a field complaint. Check edge condition, camber, and thickness tolerance on arrival, because burr height and stacking factor move core loss after the stack is built, not before. Zanesville's finishing lines are set up to meet customers' exact specifications and delivery requirements per coil, so hold each heat to that standard rather than to a typical value.
The One Check Before You Release the Order
What single check belongs in front of the order? Match the grade's directional behaviour to the machine's flux geometry. Fixed, single-axis flux — transformers, reactors, inductors with a defined path — takes RGO, which is built for exactly that alignment. Rotating flux — motors and generators — takes CRNO, whose properties hold in any direction of magnetism.
Run the check before the purchase order goes out and before the specification is frozen. It costs ten minutes and one drawing of the flux path. Skip it, and the next cost is a teardown, a requalification, and a customer who now reads your loss certificates line by line. Price cannot substitute for the check, and neither can a grade name that sounds more advanced, because the steel does not care what it costs — only which way the flux is going.
Diego Serrano
Diego Serrano is an independent stainless steel and corrosion-selection analyst covering stainless sheet, plate, coil, tube, bar, and strip. He uses ASTM A240/A240M product requirements alongside alloy chemistry, PREN, tensile properties, surface finish, sensitization risk, pitting exposure, and fabrication route. His comparison guides help designers and buyers choose grades and finishes for pressure, food-processing, architectural, marine, and general industrial service without treating all stainless alloys as interchangeable.